AI & TechnologyOctober 19, 2026
Preventive vs. Predictive vs. Prescriptive Maintenance
Preventive, predictive, and prescriptive maintenance compared: how each is triggered, the data it needs, where it fits, and how to choose a strategy per asset.
Agix International
Agix International
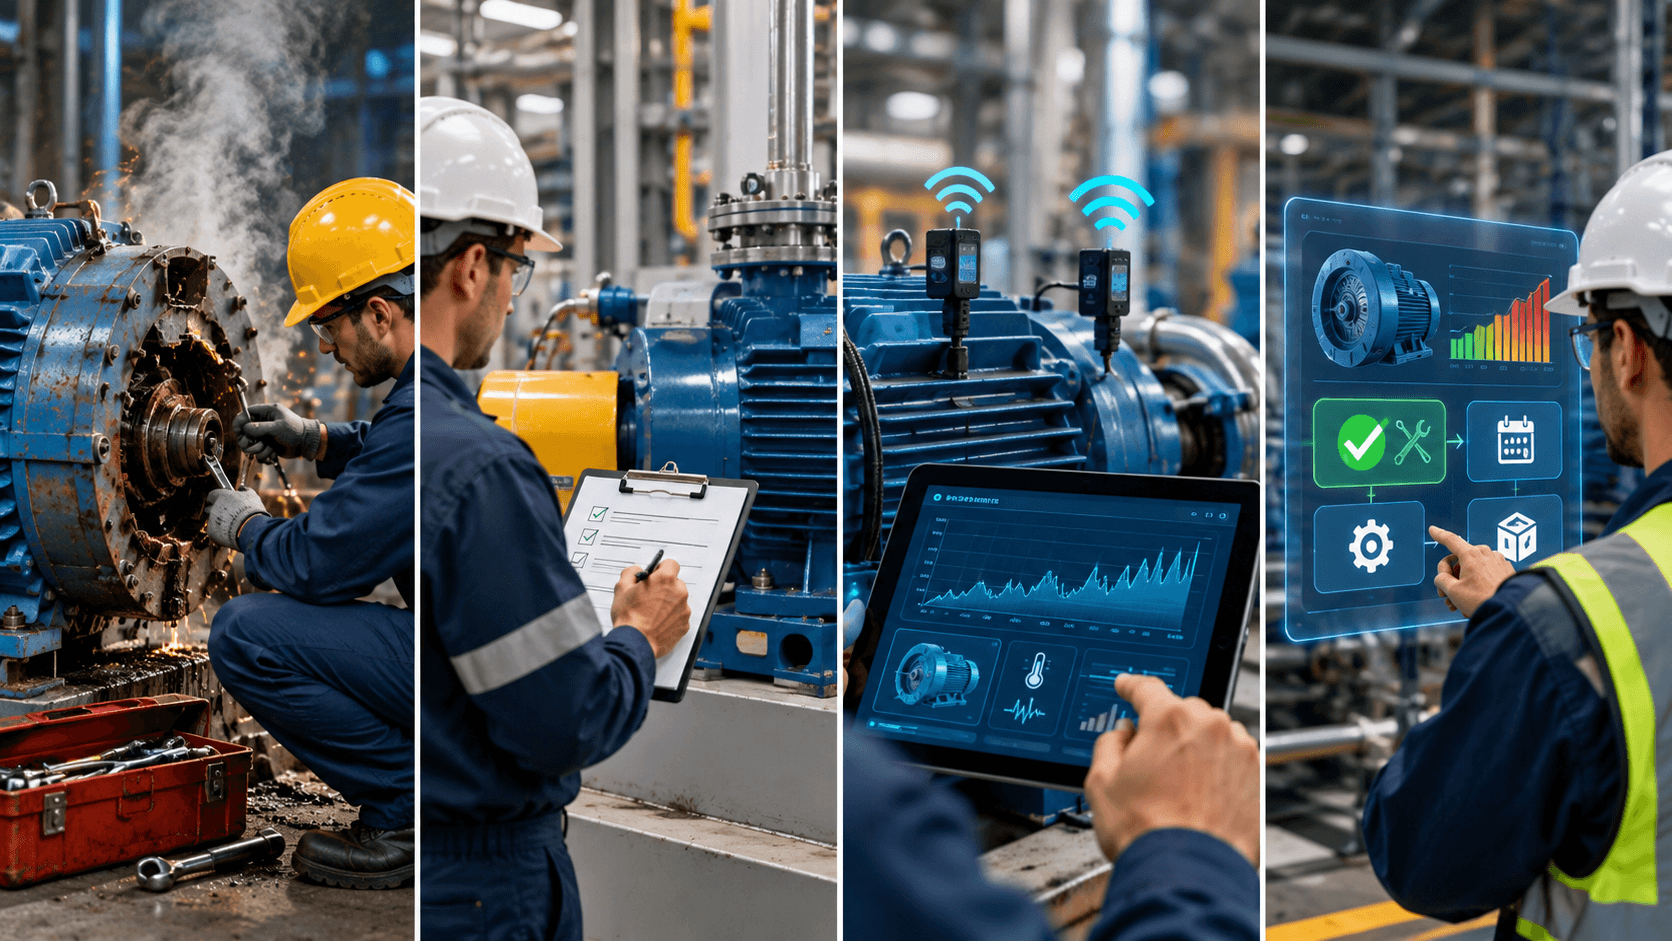
Preventive maintenance services equipment on a fixed schedule. Predictive maintenance services it when measured condition shows that a failure is developing. Prescriptive maintenance goes further and recommends what action to take and when. Most plants need all three, applied to different assets according to criticality and how detectable their failures are.
Maintenance teams are often asked to "move to predictive maintenance," as if it were a single upgrade for the whole plant. In practice, the right strategy differs from one asset to the next. A critical compressor and a lighting circuit do not deserve the same approach.
This article compares the four main maintenance strategies, including reactive maintenance, explains where each fits, and gives a simple way to choose. For the full picture of how AI enables the predictive and prescriptive approaches, see our guide to AI predictive maintenance.
The Four Maintenance Strategies
Reactive Maintenance
Reactive, or run-to-failure, maintenance fixes equipment after it breaks. It sounds careless, but it is the right choice for assets that are cheap, redundant, and quick to replace. The problem comes when it is the default for critical equipment, where every failure causes unplanned downtime, emergency labor, and expedited parts.
Preventive Maintenance
Preventive maintenance follows a schedule based on time, runtime hours, or cycles: change the oil every 500 hours, replace the belt every six months. It is simple to plan and works well for failures that are clearly tied to age or use, such as wear on consumable parts.
Its weakness is that schedules are averages. Some components are replaced while they still have plenty of life left. Others fail before their scheduled service. Every intervention also carries a risk of introducing a new fault through reassembly errors or contamination. Reliability-centered maintenance (RCM), which grew out of work in commercial aviation, established that many failures are not related to age at all, so no fixed interval can prevent them.
Predictive Maintenance
Predictive maintenance monitors the actual condition of an asset, using vibration, temperature, current, oil condition, or acoustic signals, and schedules work when the data shows degradation. It is sometimes called condition-based maintenance, although many practitioners reserve "predictive" for approaches that also forecast how much time remains.
Its value comes from the P-F interval, the time between the point when a failure becomes detectable and the point of functional failure. Good monitoring detects problems early in that window, giving planners time to order parts and schedule the repair during a convenient stop.
Prescriptive Maintenance
Prescriptive maintenance adds a recommendation to the prediction. Instead of reporting that a bearing is degrading, it might suggest reducing the load, lubricating within forty-eight hours, and replacing the bearing at the next planned shutdown, with the trade-offs of each option. It combines condition data with operating constraints, spare-parts availability, production schedules, and maintenance history.
Prescriptive systems need everything predictive systems need, plus reliable connections to planning and inventory data. They are the natural next step once predictive maintenance is working and trusted.
Side-by-Side Comparison
| Dimension | Reactive | Preventive | Predictive | Prescriptive |
|---|---|---|---|---|
| Trigger | Failure | Time, runtime, or cycles | Measured condition | Condition plus constraints |
| Data needed | Little | Asset register, schedules | Sensor data, baselines | Sensor data plus planning, inventory, and history |
| Planning horizon | None | Fixed and predictable | Weeks, depending on failure mode | Weeks, with ranked options |
| Typical systems | Work orders | CMMS or EAM schedules | Sensors, analytics, CMMS integration | Analytics, optimization, ERP and CMMS integration |
| Best suited to | Cheap, redundant, non-critical assets | Age-related wear, regulatory inspections | Critical assets with detectable failure modes | High-value fleets with complex trade-offs |
| Main risk | Costly unplanned downtime | Over-maintenance and missed random failures | False alarms and untrusted alerts | Complexity, and recommendations no one follows |
What the Benchmarks Say
Widely cited public benchmarks come from the US Federal Energy Management Program's Operations and Maintenance Best Practices guide (Release 3.0, 2010). As summarized by Pacific Northwest National Laboratory, it estimates that preventive maintenance can save 12 to 18 percent on average compared with a reactive approach, and that a properly functioning predictive program can save a further 8 to 12 percent over preventive maintenance alone.
These are averages from facility management, and they are now old. Treat them as evidence that the direction is right, not as a forecast for your plant. Your own case should be built from the downtime cost of your critical assets.
How to Choose a Strategy for Each Asset
Two questions decide most cases: how much does a failure cost, and can you detect it coming?
| Asset situation | Recommended strategy |
|---|---|
| Low failure cost, easy to replace or redundant | Reactive |
| Failure is clearly age- or usage-related | Preventive |
| Required by regulation or the manufacturer's warranty | Preventive (and add condition monitoring where useful) |
| High failure cost, failure mode gives early warning signs | Predictive |
| High failure cost, failure gives no detectable warning | Redesign, add redundancy, or apply preventive measures |
| Large fleet, complex scheduling and parts trade-offs, predictive already working | Prescriptive |
Start with an asset criticality ranking. Score each asset on safety impact, production impact, repair cost, and failure frequency. Then apply the table. The usual result is a mix: reactive for a long tail of minor equipment, preventive for age-related wear and compliance tasks, and predictive for a short list of critical machines.
Moving from Preventive to Predictive
The shift does not require replacing your preventive program overnight. A practical path:
- Pick five to ten critical assets with known, detectable failure modes.
- Instrument them with the sensors that match those failure modes.
- Run predictive and preventive side by side for a period, and compare what each would have done.
- Connect alerts to your CMMS or SAP PM so they become work orders, not just dashboard warnings.
- Extend preventive intervals on monitored assets once the predictive alerts have proven reliable.
Step 5 is where the savings appear. Until preventive tasks are actually reduced or rescheduled, predictive maintenance only adds cost.
Frequently Asked Questions
What Is the Difference between Preventive and Predictive Maintenance?
Preventive maintenance is scheduled by time or usage, whether or not the equipment needs it. Predictive maintenance is scheduled by measured condition, when the data shows that a failure is developing.
Is Predictive Maintenance Always Better than Preventive Maintenance?
No. For cheap or age-related failures, preventive maintenance is simpler and often more economical. Predictive maintenance pays off on critical assets whose failures give early warning signs.
What Is Prescriptive Maintenance?
It is maintenance guided by recommendations about which action to take and when, based on equipment condition, operating constraints, spare parts, and schedules.
Is Condition-Based Maintenance the Same as Predictive Maintenance?
They are closely related. Condition-based maintenance acts when a measurement crosses a threshold. Predictive maintenance usually also analyzes trends to estimate how much time remains before failure.
Choose the Right Strategy with Agix
Agix International builds AI, data, and enterprise system integrations that connect equipment data to maintenance planning. If you are deciding where predictive maintenance makes sense in your operations, book a consultation.
For how maintenance predictions connect to AI agents and automated workflows, see The Intelligent Enterprise Stack.